Smart Factory Implementation Challenges That Stall ROI
Smart factory initiatives promise 10–20% higher output, 7–20% lower maintenance costs, and 10–15% asset capacity gains. Yet without a structured readiness-first framework, fragmented OT data, pilot purgatory, and weak shop-floor adoption cause 65% of deployments to stall before returning measurable business value.
1. Executive Summary & Key Takeaways
Industrial enterprises are investing heavily in Industry 4.0, Industrial Internet of Things (IIoT), and smart manufacturing initiatives. Industry benchmarks from Deloitte, McKinsey, and leading automation institutes consistently demonstrate transformative potential: plants that achieve digital operational maturity experience 10–20% increases in factory output, 7–20% reductions in maintenance costs, and 10–15% improvements in asset capacity.
Yet behind these headline figures lies an uncomfortable industry reality: over 70% of digital manufacturing programs stall in "pilot purgatory." Companies install hundreds of vibration sensors, build glittering real-time Grafana dashboards, and announce AI-powered predictive maintenance initiatives—only to discover twelve months later that scrap rates have not moved, machine downtime remains unchanged, and the shop-floor operators continue tracking production using paper clipboards.
This guide examines the seven structural challenges that derail smart factory return on investment (ROI), unpacks the critical distinction between passive monitoring and closed-loop operational action, provides a practical 6-step implementation framework, and includes a downloadable readiness checklist to audit your plant before committing capital.
2. 2026 Smart Manufacturing Benchmarks
Understanding where high-performing plants pull ahead reveals why traditional manufacturing automation approaches fail in the digital era. Recent studies from industrial research bodies highlight the clear financial divide between technology-first deployments and business-led implementations:
- Productivity & Throughput: Mature digital factories unlock 10% to 20% higher overall production throughput without adding physical square footage or purchasing new heavy machinery.
- Maintenance & Asset Longevity: Transitioning from calendar-based preventative maintenance to targeted condition-based monitoring reduces equipment maintenance expenditures by 7% to 20% and slashes unplanned catastrophic breakdowns by up to 50%.
- Capacity Recovery: Eliminating micro-stoppages and unrecorded speed losses returns 10% to 15% hidden capacity back to plant managers, deferring millions in capital expansion.
- Operational & Cyber Risk: Concurrently, 65% of industrial facilities identify cybersecurity vulnerabilities, fragmented proprietary protocols, and lack of trained OT/IT personnel as severe threats to project continuity.
The takeaway is decisive: smart manufacturing creates immense enterprise value, but the margin between transformative ROI and stalled capital spending depends almost entirely on foundational operational readiness.
3. Why Smart Factories Fail to Show ROI
Why do multi-million-dollar digital manufacturing initiatives frequently fail to translate into balance-sheet value? Research across hundreds of manufacturing deployments reveals a consistent failure pattern: organizations treat smart manufacturing as an IT software procurement exercise rather than an operational transformation.
When plants install sensors without fixing foundational workflow constraints, they encounter the classic "Pilot Purgatory" warning signs:
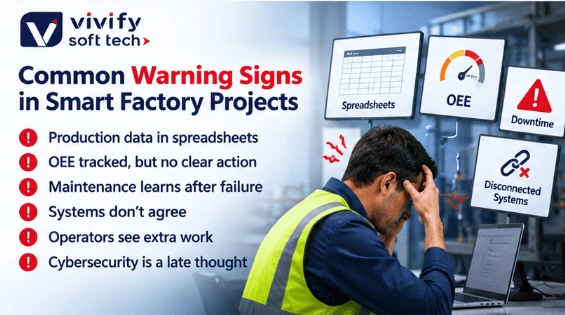
Production Data in Spreadsheets
01Isolated shift records reconciled manually in Excel.
OEE Tracked Without Action
02Dashboards show downtime but trigger no floor intervention.
Maintenance Learns After Failure
03Lack of condition-based alerts causes sudden stoppages.
Systems Disagree
04Disconnected PLC, SCADA, ERP, and MES records yield conflicting numbers.
Operators Burdened
05Floor workers see extra administrative data-entry work.
Cybersecurity as a Late Thought
06Exposed OT networks invite catastrophic ransom risk.
As illustrated above, smart factory initiatives fail primarily when three foundational gaps are left unaddressed:
| Operational Dimension | Traditional Plant Baseline | Smart Factory Target State | The Stall Risk (Root Cause) |
|---|---|---|---|
| Business Case | Manual logs, anecdotal downtime reports | Workload-level financial payback models | Procuring platforms without a defined bottleneck KPI |
| Data Architecture | Isolated PLC registers, manual Excel tallying | Unified MQTT / OPC-UA industrial data bus | High data noise, missing timestamps, asynchronous packets |
| Shop-Floor Adoption | Whiteboards, clipboard shift handovers | Operator-assist touch tablets & mobile alerts | Top-down surveillance perception; operators bypass system |
| OT/IT Security | Air-gapped flat networks, unpatched HMIs | ISA/IEC 62443 zoned zero-trust architectures | Connecting legacy PLCs to enterprise IT triggers cyber lockdowns |
When leadership fails to bridge these operational gaps prior to deploying hardware, smart factory projects incur heavy recurring software subscription costs and engineering fees long before the factory floor sees any tangible operational improvement.
4. The 7 Core Challenges That Stall Smart Factory ROI
Based on comprehensive analysis of manufacturing deployments across discrete, batch, and continuous process industries, seven specific hurdles repeatedly stall ROI. Below is the detailed breakdown of each challenge along with the validated practical fix.
No Clear Business Case or Bottleneck Priority
Many smart factory programs begin with an executive mandate to "digitize the factory" or "install IIoT." Teams procure generic cloud IoT platforms and instrument random machinery without first identifying the plant's binding production constraint. When data finally streams into cloud dashboards, management cannot tie the expenditure to a single dollar saved or additional unit shipped.
Common symptoms include:
- Instrumenting non-bottleneck machines that have excess buffer capacity, producing zero throughput gain.
- Lack of baseline financial metrics (e.g., precise cost per minute of line stoppage).
- No designated operational owner accountable for realizing savings.
Apply the Theory of Constraints: Start by mapping your plant's single binding bottleneck. Identify the machine or cell that directly restricts total plant revenue. Calculate the precise financial cost of 1% downtime on that cell, and tie the initial IIoT business case strictly to opening that specific bottleneck.
Fragmented Manufacturing Data & Legacy Protocol Silos
A single plant floor often houses machines built over four decades: 1980s relay-logic stamping presses, 1990s Siemens S7-300 PLCs using Profibus, 2010s Allen-Bradley ControlLogix running Ethernet/IP, and modern CNC machines outputting MTConnect. Incompatible communication standards create severe data silos where telemetry cannot be correlated across production stages.
When raw data is dumped into cloud data lakes without context, teams suffer:
- Inconsistent timestamp synchronization making root-cause sequence tracing impossible.
- Unstandardized register tag names (e.g.,
Line1_Spindle_RPMvsL01_SPD_ACTUAL). - High edge network bandwidth bills from transmitting raw 1 kHz vibration noise rather than edge-computed features.
Deploy Edge Protocol Converters & Unified Namespaces: Install intelligent edge gateways running standard OPC-UA and MQTT Sparkplug B brokers. Map all machine registers into a standardized ISA-95 hierarchical model (Enterprise > Site > Area > Line > Work Cell > Asset) before transmitting telemetry to enterprise databases.
Treating OEE as a Vanity Dashboard Rather Than an Action Engine
Overall Equipment Effectiveness (OEE) is the universal manufacturing KPI: Availability × Performance × Quality. However, many plants treat OEE as a historical wall-mounted scorecard that executives review during weekly retrospectives. Knowing that yesterday's OEE was 64% does nothing to prevent the 45-minute tooling jam happening right now on line 3.
Key pitfalls in OEE implementations:
- Relying on manual operator downtime reason entry, which defaults to generic "operator lunch" or "material wait."
- Ignoring micro-stoppages (10–30 second jams) that evade manual logs but collectively consume 12% of shift capacity.
- Failing to trigger automated, real-time maintenance dispatch when speed drops below 85% of rated nameplate speed.
Automate OEE Telemetry with Real-Time Interventions: Calculate OEE automatically using PLC cycle counters and photo-eye sensors. Configure automated escalation rules: if a critical bottleneck machine drops below target speed for 3 consecutive minutes, dispatch an instant SMS/push notification directly to the line technician.
Predictive Maintenance Without an Underlying Maintenance Strategy
Predictive Maintenance (PdM) is frequently marketed as a plug-and-play AI silver bullet. Companies install triaxial accelerometers on every motor, expecting algorithms to predict failures weeks in advance. However, without a clean history of component failure modes, lubrication logs, and standardized operating conditions, machine learning models generate continuous false-positive alerts that technicians quickly learn to ignore.
Establish Condition-Based Baselines on Critical Assets Only: Before deploying complex neural networks, conduct an asset criticality assessment. Place high-resolution vibration and thermal sensors solely on Tier-1 assets. Establish simple statistical threshold alarms (ISO 10816 vibration severity standards) and ensure your CMMS can automatically generate work orders from telemetry triggers.
Poor Shop-Floor Adoption & Change Resistance
When smart factory tools are designed by corporate IT without input from shop-floor operators, workers view the system with intense suspicion—as digital surveillance designed to police their bathroom breaks. If the interface is complex, requires typing on small screens with greasy gloves, or adds administrative burden to an already demanding shift, operators will actively circumvent it or enter bogus data.
Design for the Frontline Worker: Involve machine operators and maintenance supervisors in initial UI mockups. Replace manual data entry with one-tap touchscreen categorizations. Eliminate physical paperwork so digital tools save operators time rather than adding overhead. Reward operators who proactively log root-cause issues.
Cybersecurity Treated as an Afterthought
For decades, operational technology relied on "security through obscurity" and physical air-gaps. Connecting factory networks to cloud analytics exposes legacy PLCs running unencrypted, unauthenticated protocols (e.g., standard Modbus or S7comm) to external threats. A single infected laptop plugged into a maintenance port can propagate ransomware across the plant floor, causing total production shutdowns that dwarf any projected IIoT efficiency gains.
Enforce ISA/IEC 62443 Micro-Segmentation: Segment shop-floor networks using industrial firewalls into defined security zones and conduits. Never route raw PLC traffic across the public internet. Use outbound-only MQTT connections through hardened edge DMZs, and require multi-factor authentication for all remote engineering access.
Trying to "Boil the Ocean" (Pilot Purgatory)
The final and most pervasive trap is attempting a monolithic digital transformation across multiple plants simultaneously. Organizations spend 18 months evaluating 10 different IoT software vendors, write exhaustive multi-hundred-page RFPs, and attempt to instrument 50 lines at once. As implementation timelines stretch and costs compound without demonstrable wins, executive sponsorship evaporates and the project is abandoned.
Adopt a "Lighthouse Cell" Methodology: Select one production line, one critical machine cell, and one quantifiable operational problem. Deliver measurable, verified ROI in under 90 days. Use that validated financial win and operational blueprint to self-fund and scale across subsequent lines.
5. The OEE Reality Check & Action Matrix
Overall Equipment Effectiveness is frequently misunderstood. A world-class OEE benchmark of 85% sounds straightforward, yet a plant with 90% Availability, 90% Performance, and 90% Quality achieves an OEE of only 72.9%(0.90 × 0.90 × 0.90 = 0.729). The multiplication compound effect means even small losses across each pillar severely penalize total plant profitability.
| OEE Pillar | The Six Big Losses | Traditional Monitoring (Passive) | IIoT Closed-Loop Intervention (Active) |
|---|---|---|---|
| Availability | Equipment Failures & Setup/Adjustments | End-of-shift paper logs; "machine stopped 45 min" | PLC stops trigger instant tech dispatch; automated changeover timer |
| Performance | Idling / Minor Stoppages & Reduced Speed | Undetected; recorded as normal production shift | Optical sensors detect 15-second jams; speed drops flag lubrication need |
| Quality | Process Defects & Reduced Yield | End-of-line QA inspection bins scrapped parts | In-line vision inspection rejects defect at source; halts bad feed batch |
To convert OEE data into ROI, plant teams must transition from passive retrospective analysis to automated telemetry-driven workflows. When abnormal vibration or cycle latency triggers a targeted work order before catastrophic tooling failure, the smart factory delivers measurable financial returns.
6. Asset Criticality & Sensor Selection
A common cause of budget overruns is over-instrumenting low-impact machinery. Deploying expensive high-frequency accelerometers and edge processors on a redundant cooling fan yields virtually zero payback. Modern reliability engineering categorizes shop-floor equipment into three distinct tiers:
Critical Assets
Single points of failure with no redundant backup. Failure halts total plant output (e.g., main stamping press, paint booth curing oven, primary extruders). Strategy: Continuous edge vibration, current, and temperature telemetry with automated shutdown interlocks.
Essential Assets
Equipment with partial buffer capacity or shared workload units (e.g., CNC milling banks, packaging conveyors). Failure reduces throughput but allows degraded operations. Strategy: Periodic wireless sensor bursts (every 10–15 min) tracking thermal trends and run-hours.
Non-Critical Assets
Low-cost, redundant, or easily replaceable components (e.g., standard sump pumps, exhaust fans, manual assembly fixtures). Failure carries negligible business impact. Strategy: Run-to-failure or standard visual route inspections. Do not instrument with costly IIoT hardware.
7. The 6-Step Implementation Framework
To transition from ad-hoc technical experiments to a self-funding digital manufacturing program, leadership must enforce a structured implementation methodology. The framework below coordinates business value, technical architecture, and shop-floor change management.
Successful smart factories synchronize six critical pillars before scaling:
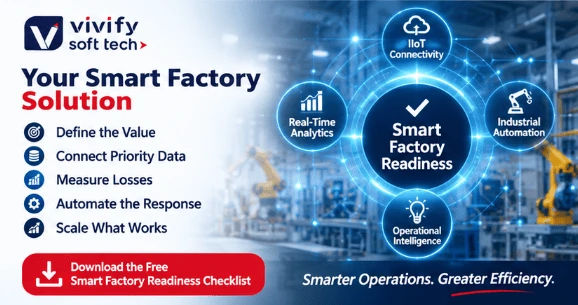
Business Value
01Target the single binding bottleneck with defined ROI targets.
Data Foundation
02Standardize edge gateways and ISA-95 namespaces.
Pilot Line
03Prove verified financial returns on a lighthouse cell within 90 days.
Change Management
04Equip operators with intuitive, touch-friendly digital tools.
Security-by-Design
05Enforce ISA/IEC 62443 zone segmentation across IT/OT.
Scaling & Governance
06Replicate modular blueprints factory-wide with FactorAI.
Business Value Definition
Define the single highest-cost production bottleneck. Calculate the baseline financial impact of unplanned downtime, scrap, or bottleneck cycle latency before procuring sensors.
Download the Vivify Smart Factory Readiness Checklist
Assess your plant's readiness across business case alignment, PLC/SCADA connectivity, shop-floor adoption, and cybersecurity posture before committing capital. Use this rigorous 6-part audit framework to identify critical gaps that stall smart factory ROI.
9. Where Vivify Soft Tech Fits
Once the business bottleneck, data foundation, and value case are clearly established, selecting the right implementation engineering partner ensures that your plan translates into a robust, high-availability system. Vivify Soft Tech engineers end-to-end industrial automation and smart-factory platforms designed to integrate with existing plant equipment rather than forcing expensive rip-and-replace disruptions.
PLC & SCADA Integration
Connect legacy and modern PLCs (Siemens, Rockwell, Mitsubishi, Omron) using standardized edge gateways, OPC-UA, and MQTT Sparkplug B brokers without modifying critical machine safety logic.
FactorAI Manufacturing Platform
Vivify's unified manufacturing intelligence suite brings together production ERP, real-time MES, machine monitoring, predictive maintenance, quality control, and robotic automation under one pane of glass.
Real-Time OEE & Downtime Tracking
Automate availability, performance, and quality telemetry with sub-second accuracy. Eliminate manual clipboards and dispatch instant mobile alerts to technicians when lines deviate from optimal throughput.
Secure IT/OT Convergence
Architect resilient ISA/IEC 62443 zone-and-conduit boundaries, industrial DMZs, and role-based access controls to connect shop-floor telemetry to cloud enterprise analytics without compromising operational integrity.
10. Conclusion & Strategic Next Steps
Smart factory ROI does not fail because sensors, dashboards, or AI algorithms lack transformative potential. It stalls when initiatives are decoupled from genuine production bottlenecks, reliable data foundations, accountable cross-functional teams, and measurable business outcomes.
The highest-performing industrial enterprises adhere to a disciplined rollout sequence: start small on a lighthouse bottleneck line, prove verified financial payback, integrate machine telemetry securely, engage frontline operators as partners, and scale with a repeatable operating model.
If your plant is experiencing disconnected systems, unreliable OEE figures, recurring unpredicted breakdowns, or low adoption of digital tools, a structured readiness assessment is the safest, most cost-effective first step.
11. Frequently Asked Questions (FAQs)
The most common challenges are unclear business goals, disconnected IT and OT systems, poor data quality, weak shop-floor user adoption, cybersecurity risks, legacy equipment protocol incompatibility, and lack of value tracking. These issues prevent smart-factory investments from producing measurable ROI.
Need an IIoT & OT Architecture Review?
Connect with Vivify's industrial IoT architects to bridge the IT/OT divide, automate OEE telemetry, and scale connected manufacturing with FactorAI.
Request Architecture Review